Get in touch with Welong Company
Forged Shafts Heavy-Duty Steel
Custom Steel Shaft Forging — Carbon, Alloy & Stainless Grades to API / ASTM / ASME / DIN / GB
Why forged shafts outperform cast and bar-stock shafts. In forged shafts, forging helps align the metal’s grain flow along the load path.
- Straight, step, flanged and hollow-bored profiles
- Carbon, alloy and stainless steel, plus aluminum, copper, titanium and zirconium grades
- API, ASTM, ASME, DIN and GB documentation on request
We build these for power, mining and heavy machinery programs where an unplanned shaft replacement stops the whole line — and Welong’s casting and forging division has supplied that customer base since 2001, with in-house heat treatment and non-destructive testing.
0.2–50T
Weight range
7
Material families
6
Standards Spec
9
QC incl. UT+MT
3
Forging Methods
2001
Operating Since
When Cast or Machined Shafts Fail Under Load, How Forging Solves It
A forged shaft is formed by compressive plastic deformation, which aligns the steel’s internal grain structure along the shape of the part instead of leaving it randomly oriented as in a casting. That continuous grain flow is what gives a forged shaft its fatigue resistance under the cyclic torque and bending loads a rotating shaft sees every cycle it turn.
Where the Alternatives Fall Short
- Cast shafts: shrinkage porosity and uneven grain size sit inside the part, invisible until an ultrasonic scan – or a failure – finds them
- machined bar stock: avoids porosity but cuts across the material’s natural fiber flow at every step and shoulder, which is exactly where fatigue cracks like to start
The real cost of a shaft failure rarely shows up on the original purchase order – it shows up in emergency freight for a replacement, in secondary damage to a coupling or bearing housing, and in the production hours lost while the line is down. That’s why total cost of ownership, not unit price, is the number that should drive the material and process decision.
Why This Matters on Your Line
- Continuous grain flow follows the shaft’s external contour through steps, flanges and shoulders
- No internal shrinkage voids or gas porosity from a solidification process
- Heat treatment after forging tunes hardness and toughness for the specific duty cycle
- Our forging process runs the full sequence in-house: forge to your drawing in carbon, alloy or stainless steel, then machine, heat-treat and test before the shaft ship. The sections below walk through material selection, how forging compares to casting and machined bar stock, and what to expect from a Welong quote.
Forging Methods We Use
- Open-die forging works the billet between flat or simple-contoured dies under repeated press strokes – the standard method for large, simple-profile shafts and step shafts where a closed die isn’t economical
- Closed-die forging forms the billet inside a die cavity that matches the finished shape more closely, reducing machining stock on complex profiles
- Roll forming suits shaft sections and rings where progressive rolling produces the required cross-section more efficiently than die forging
- forging process innovations continue on two fronts: US Patent 8,210,018 describes a drop-forging die that yields better rib-height-to-base-width ratios for compensation shafts, and WO2013093285A1 simplifies subsequent machining by drilling a turbomachine shaft’s billet prior to forging. shaft geometry, volume, and required finish-machining allowance will determine whether the method is the hot, cold, or warm-forging type, so your part’s drawing-rather than just reference, such as hot/cold or closed/open die-determines the method for your particular order.
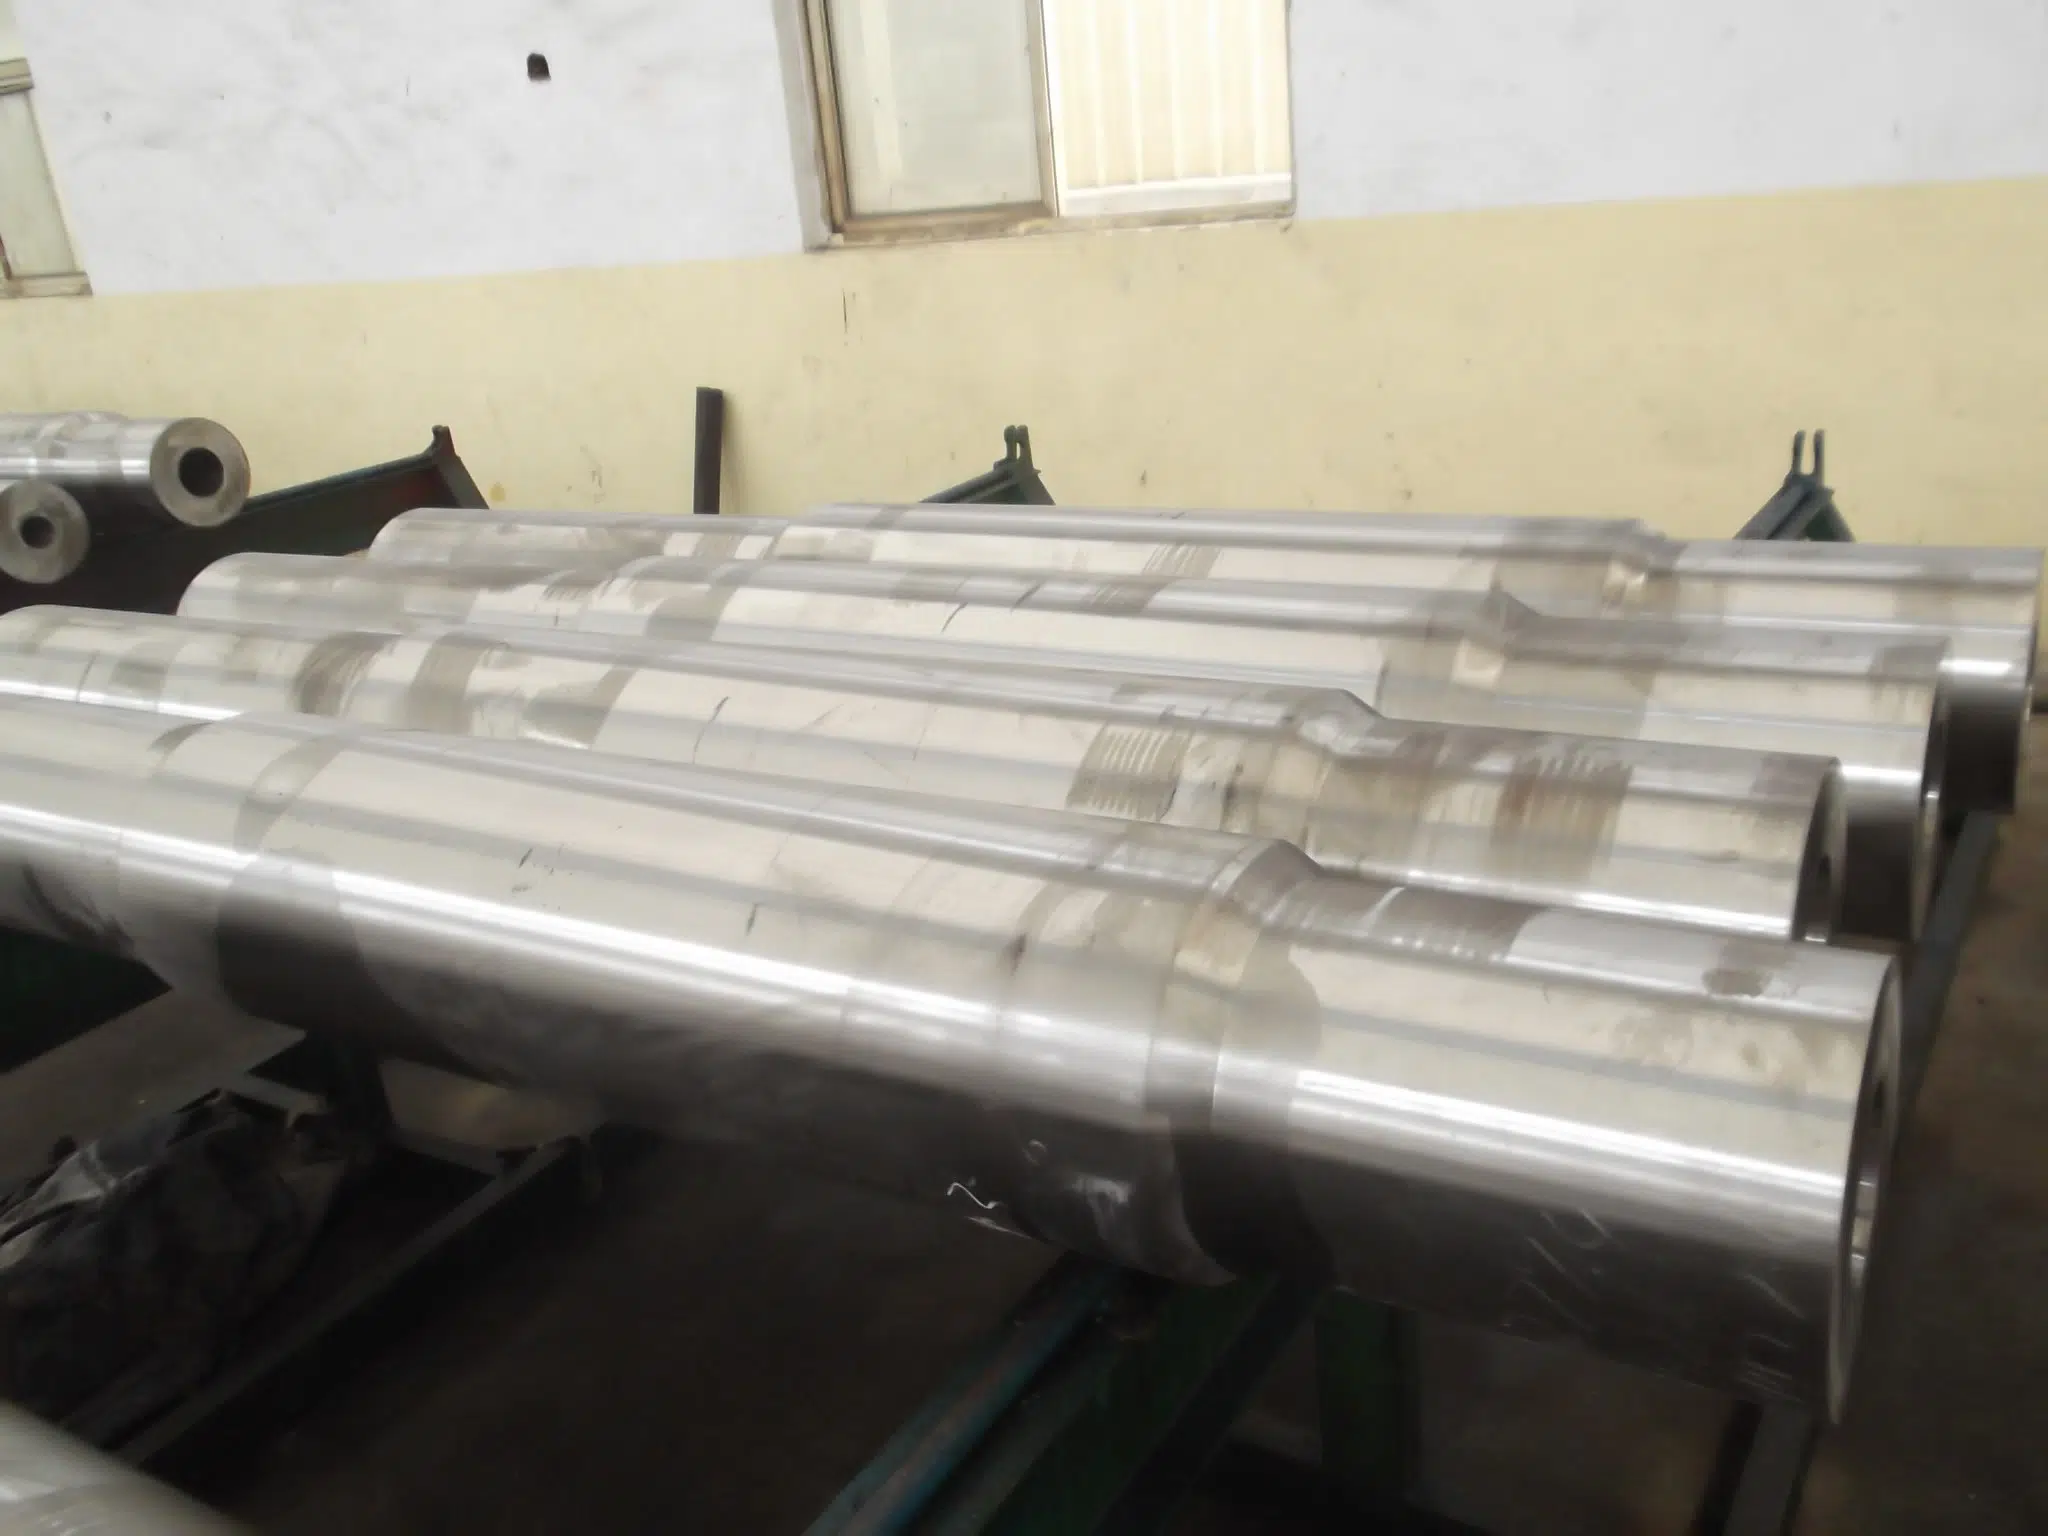
Welong Forged Shaft Range, Types & Material Selector
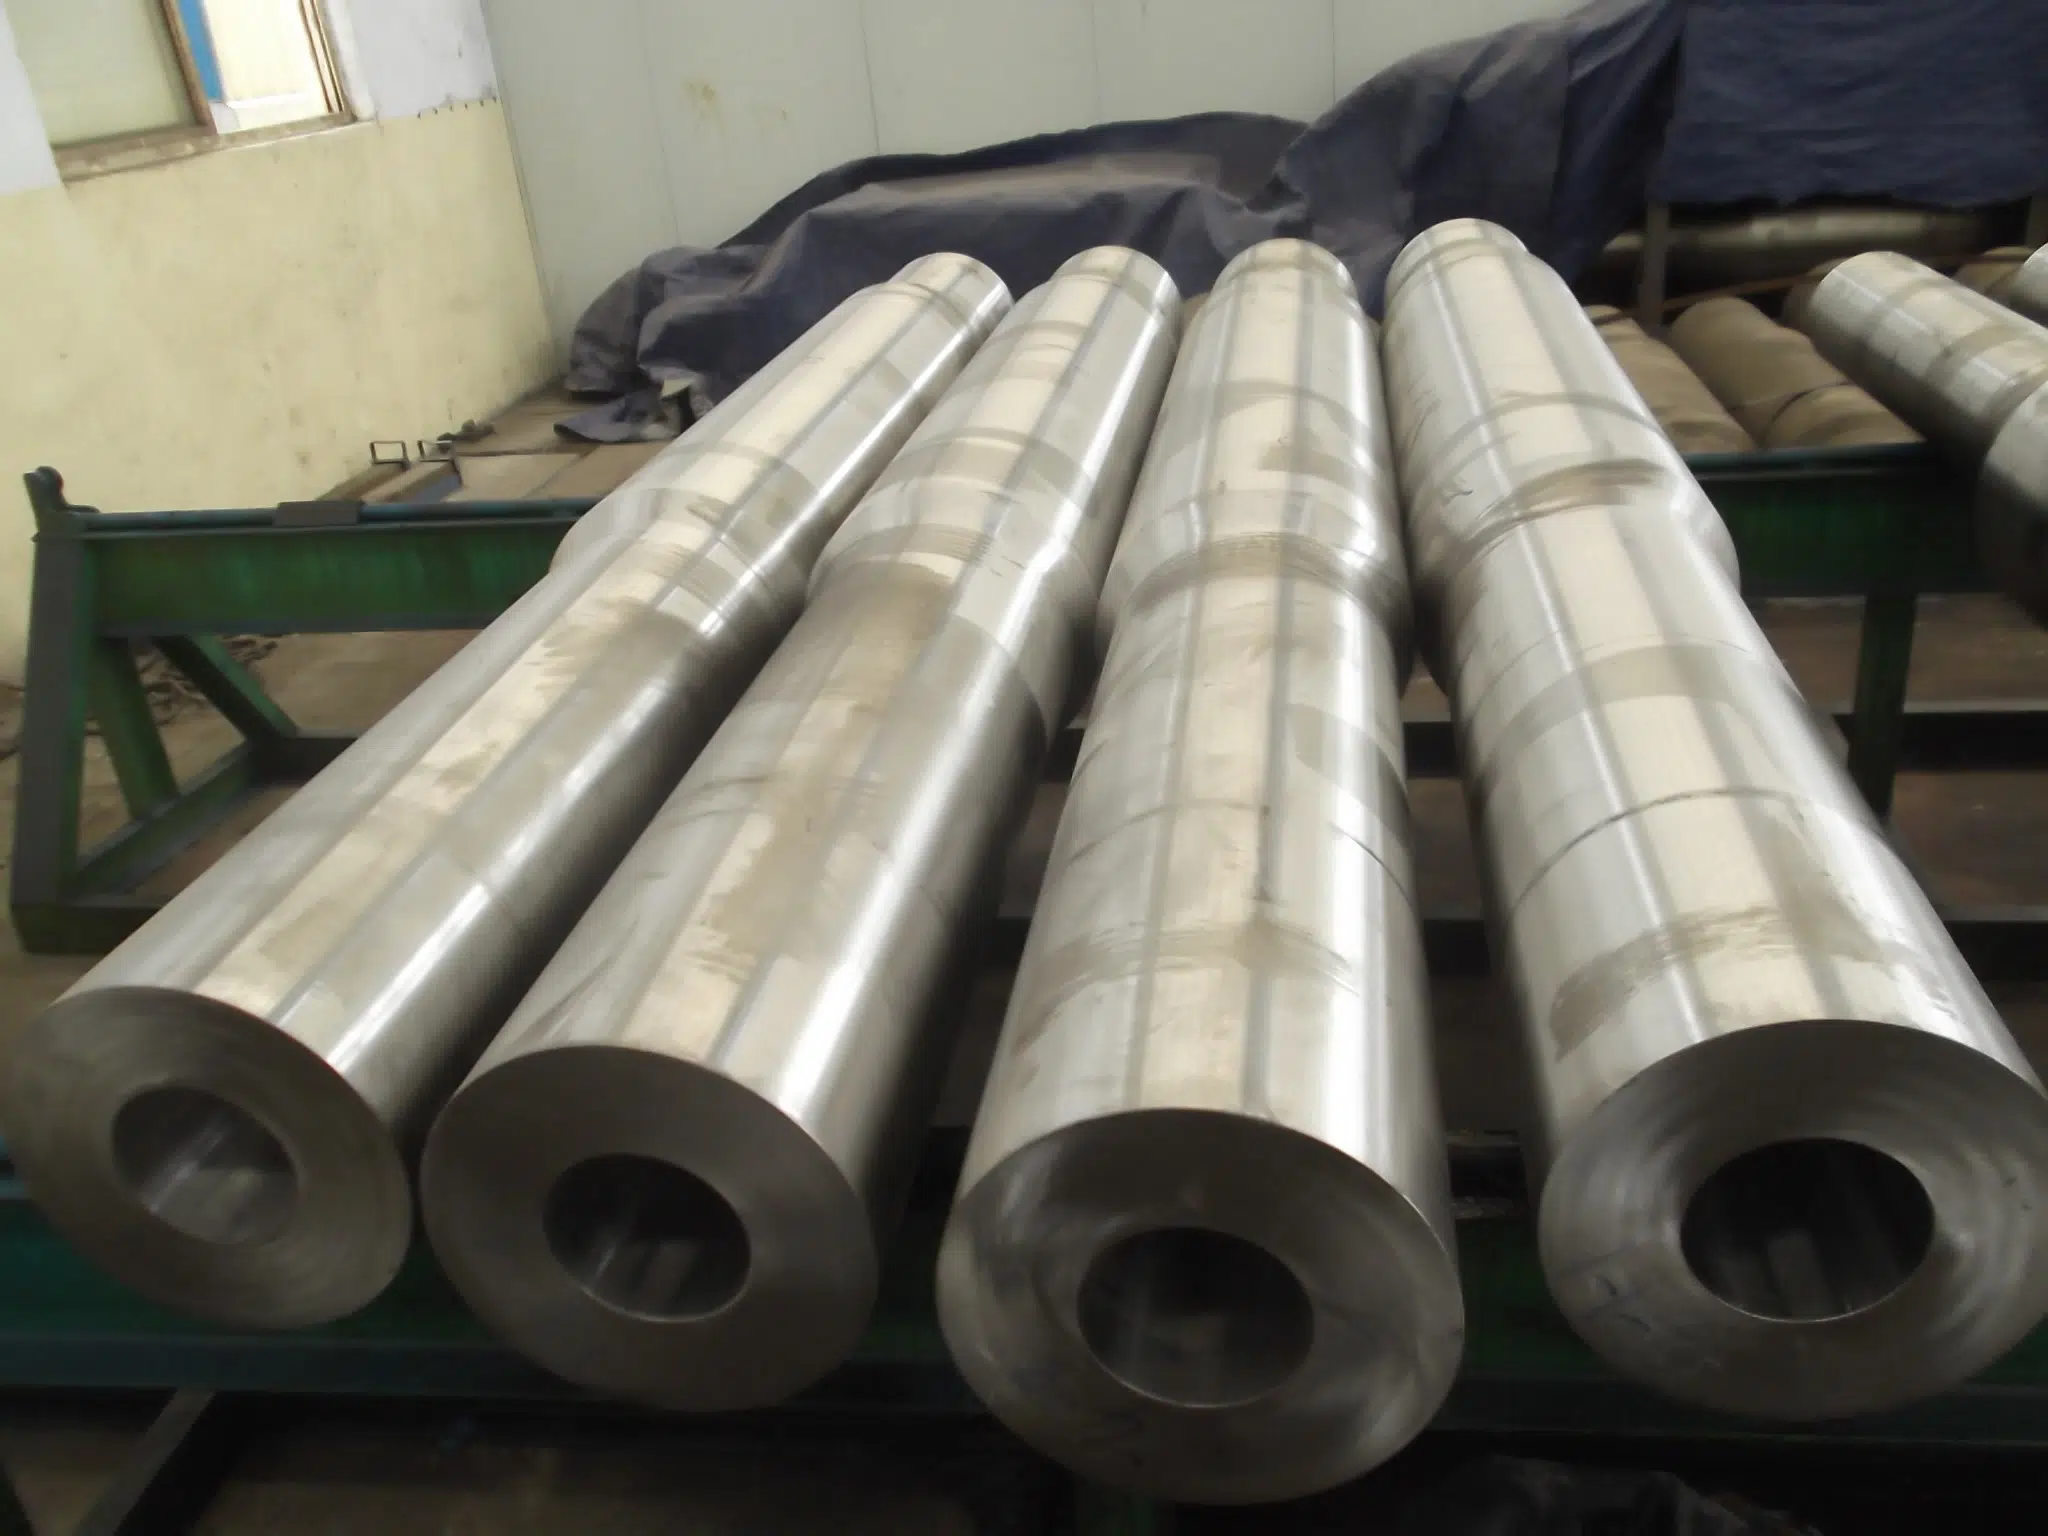
We forge four types of shafts: straight, step (multiple diameter transitions), flanged, and hollow-bored for weight-critical applications or fluid-carrying ones. Forged crankshafts, forged rotor shafts and forged step shafts for pinion applications come as step- or flanged- shaft variants based on the customer’s drawing-as do custom forged parts such as flanges and rings.
Engineering Note, Material Selection
Carbon steel is specified for general-purpose shafts when the cost is more critical than corrosion resistance — the international specification for these non-alloy forging grades is ISO 683-1, which covers hammer- and drop-forged non-alloy steels for quenching and tempering. High-performance alloy steel grades such as 42CrMo4, 4140, and 4340 impart strength and hardenability for demanding, high-torque, high-cycle applications.
| Material | Duty | Key Property | Common Application |
|---|---|---|---|
| Carbon steel | General industrial, moderate load | Cost-efficient, good machinability | Conveyor drive shafts, general transmission |
| Alloy steel (42CrMo4 / 4140 / 4340) | High-torque, cyclic loading | High hardenability, fatigue resistance after Q&TM | Mill main shafts, gearbox shafts, rotor shafts |
| Stainless steel | Corrosive or hygienic environments | Corrosion resistance | Process equipment, marine-exposed shafts |
| Aluminum alloy | Weight-critical, moderate load | High strength-to-weight ratio | Light transmission shafts, mobile equipment |
| Copper alloy | Conductivity or bearing-surface duty | Wear and galling resistance | Bushings-adjacent shaft sections |
| Titanium / Zirconium | Extreme corrosion or aerospace-grade duty | Corrosion resistance at high strength | Specialty chemical processing, aerospace-adjacent components |
Every forged shaft quotation is tailored to your drawing so that your tolerance, keyway, thread, and surface finish specifications (including painting, galvanizing, or powder coating) are confirmed prior to setting your forging schedule, rather than just assuming a match based on catalog sizes. Those same material-and-process controls-including heat treatment, testing and inspections-apply to shafts headed to steel mills, power-generation programs, or automotive and aerospace-adjacent industrial applications, where high-quality, repeatable output and long-term durability are paramount.
Shaft Dimensions
Welong’s forging capabilities span 0.2 to 50 ton weight range, encompassing smaller transmission shafts up to larger mill and turbine shafts. The required process depend on your part’s diameter, length, and weight relative to that tonnage range-discuss this with your contact when sending your drawing and compare to our latest forging schedule for realistic lead time assessment, as process is dependent on geometry as well as tonnage.
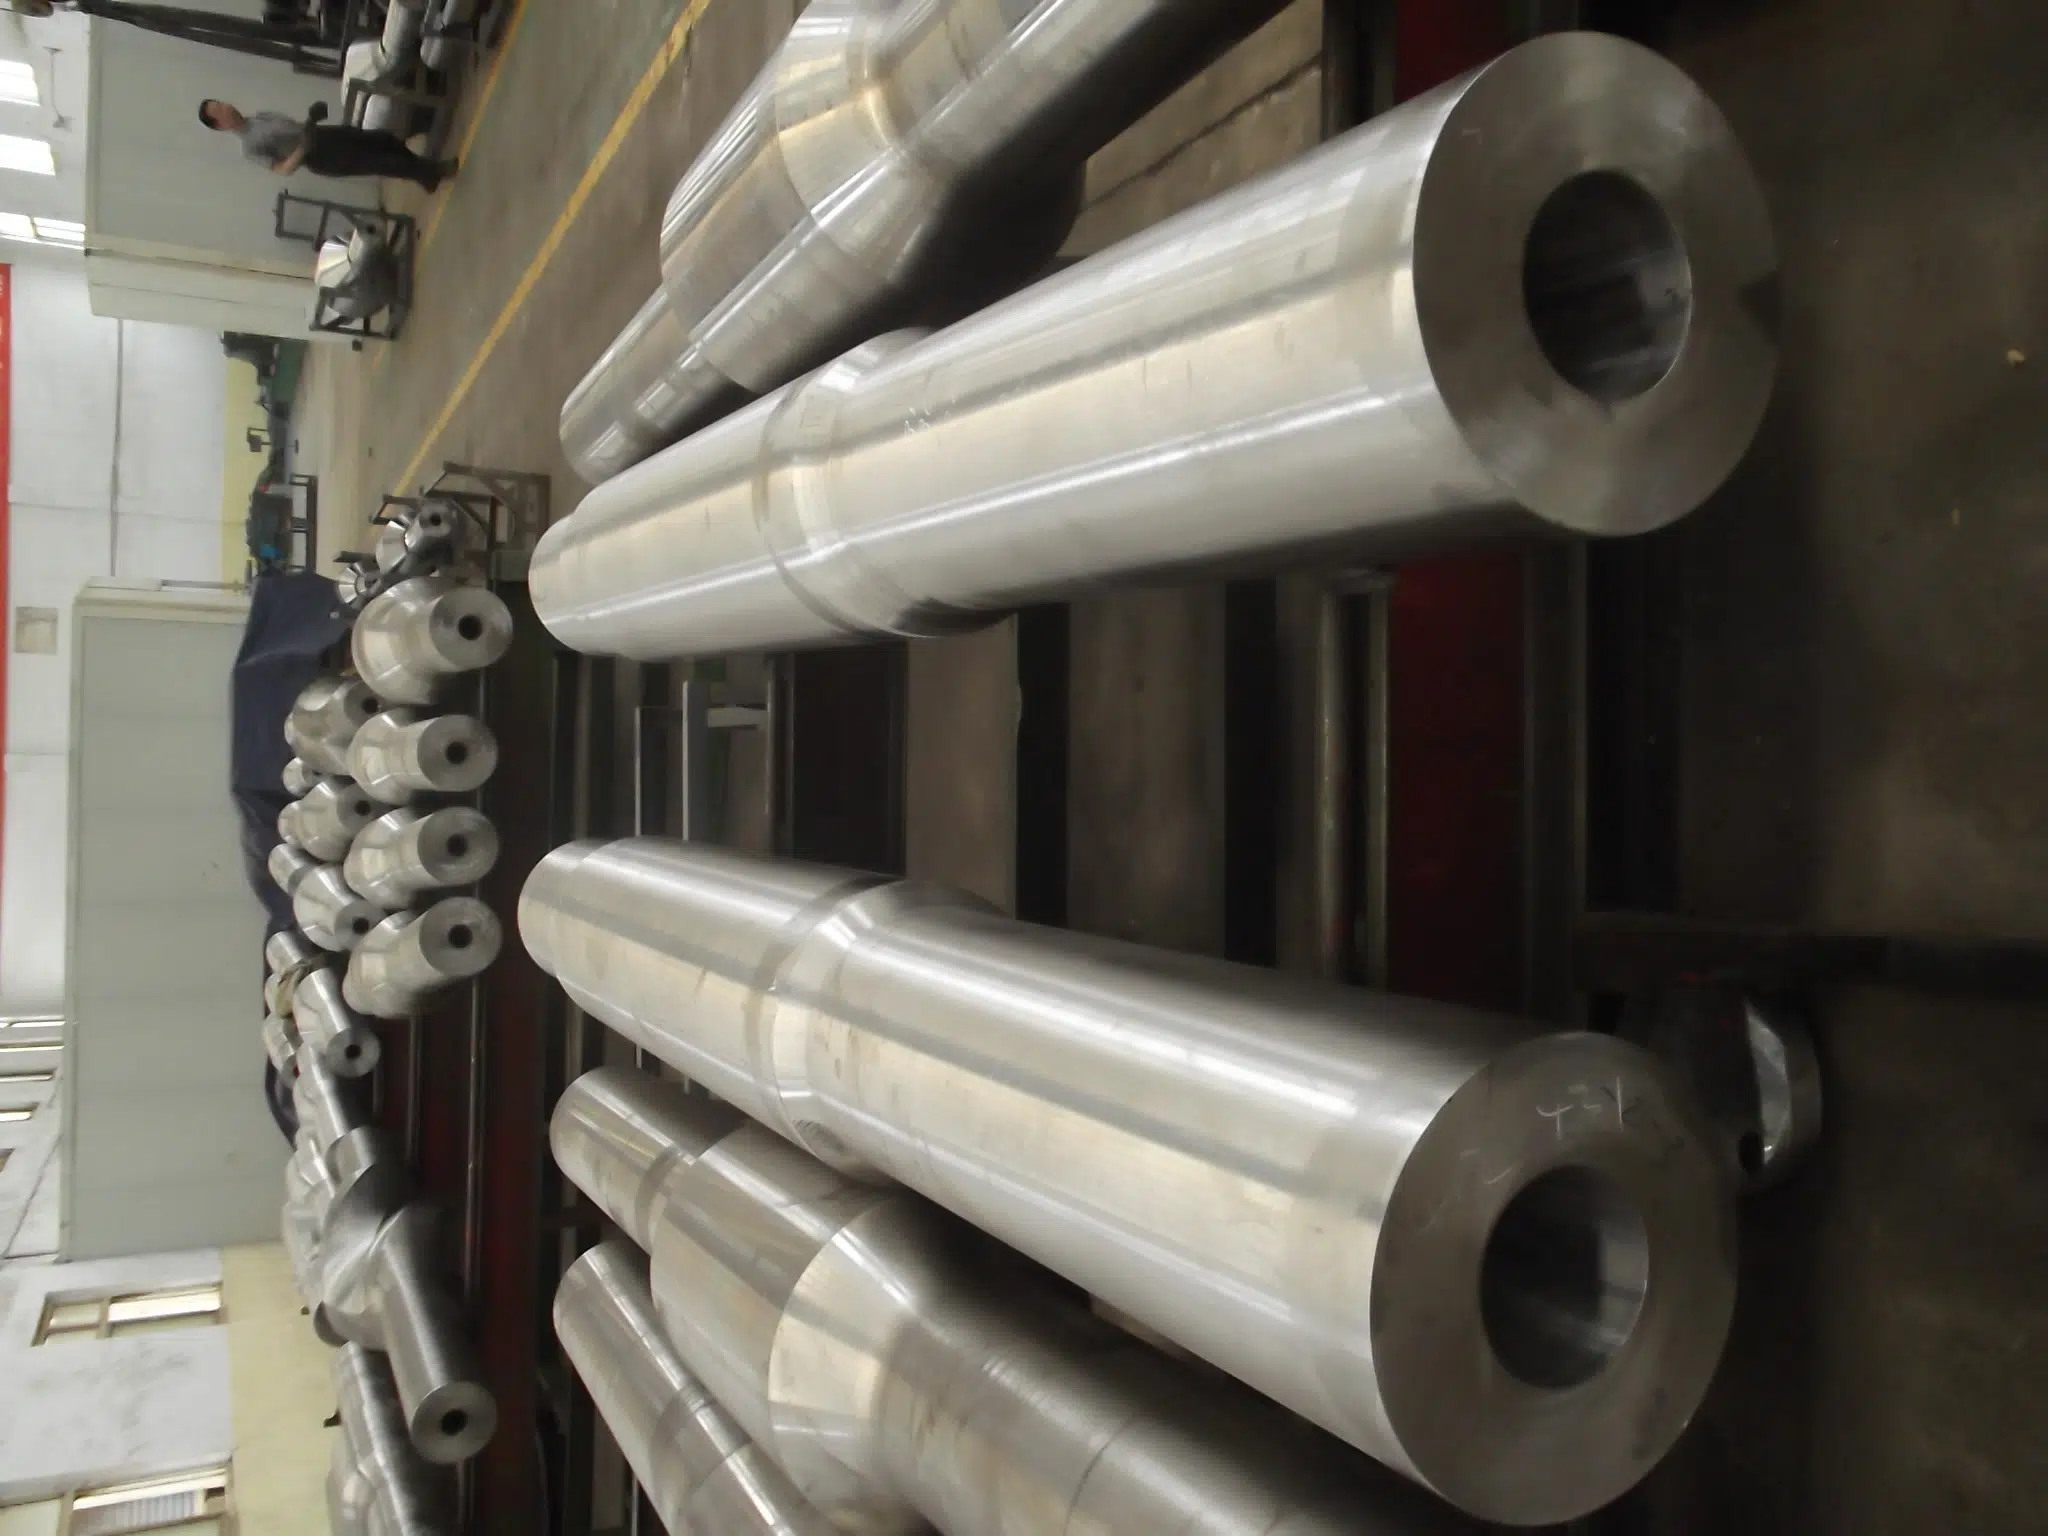
Shop-floor product record
Real Forged Shaft Components from Production
Finished and semi-finished forged components are shown as production evidence near the material selector, helping buyers inspect shaft surface, machined ends and shop-floor scale. Total added photos: 5.
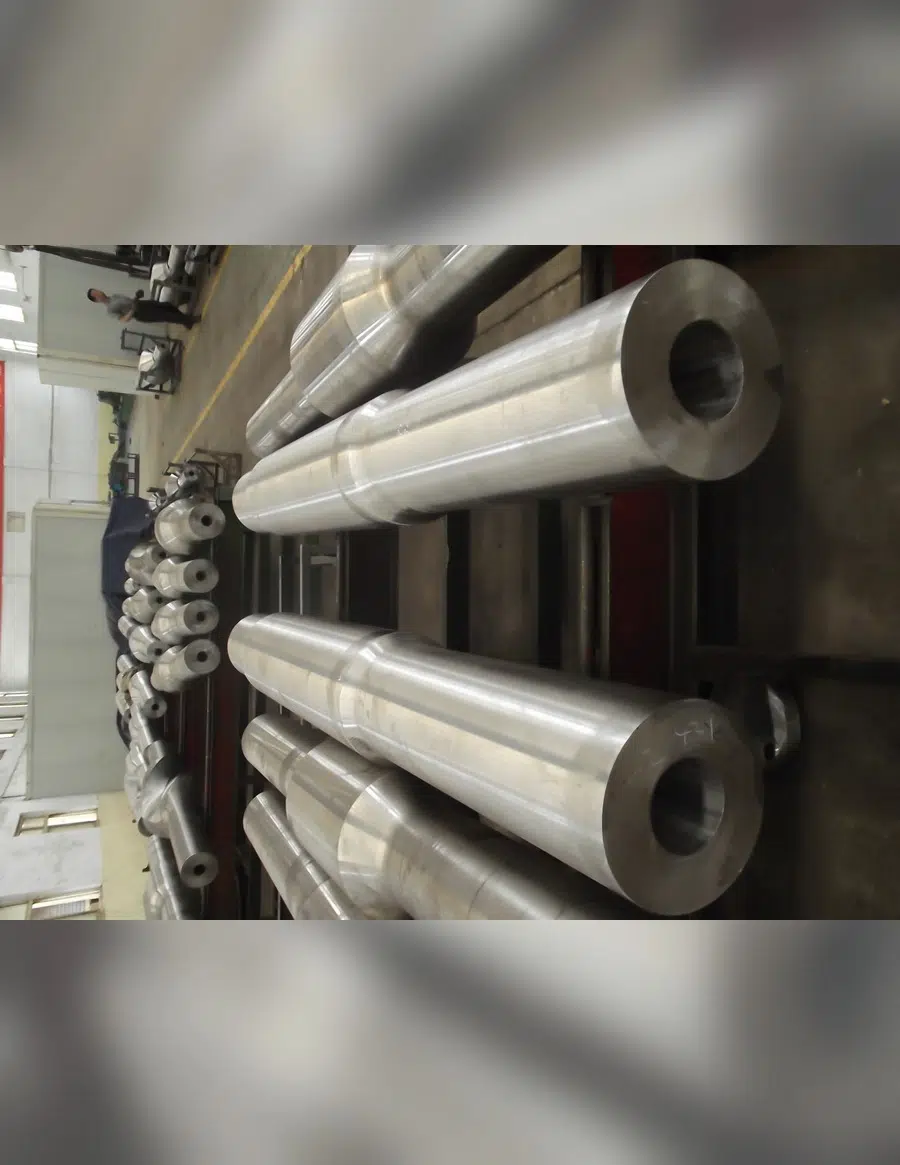
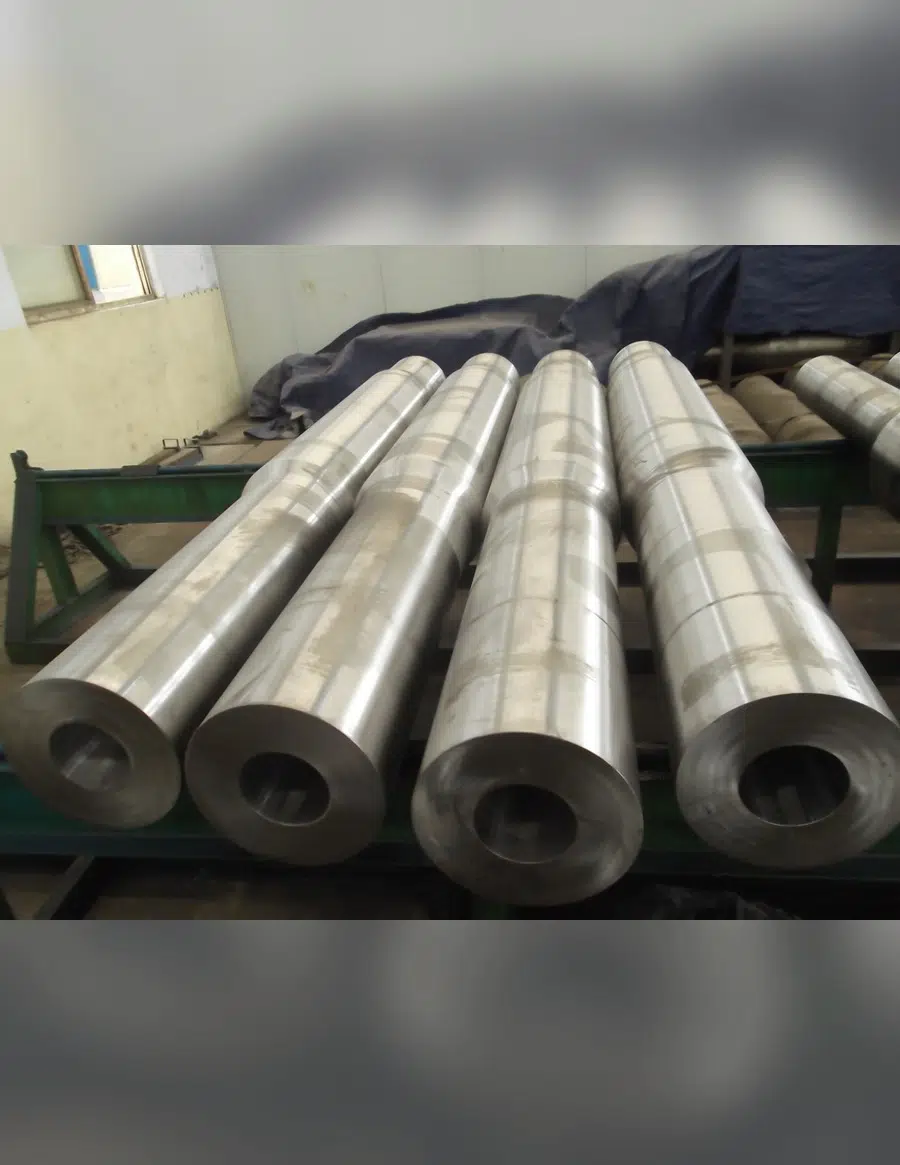
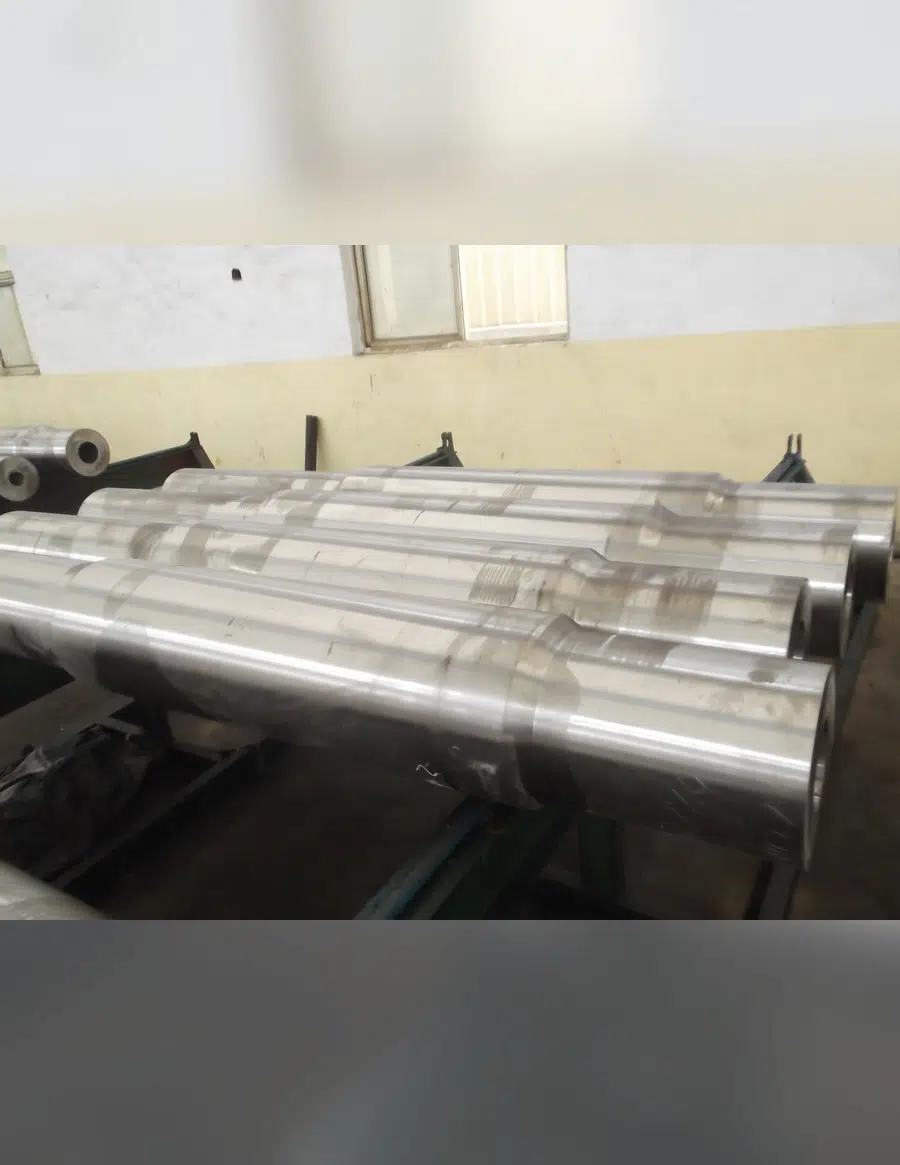
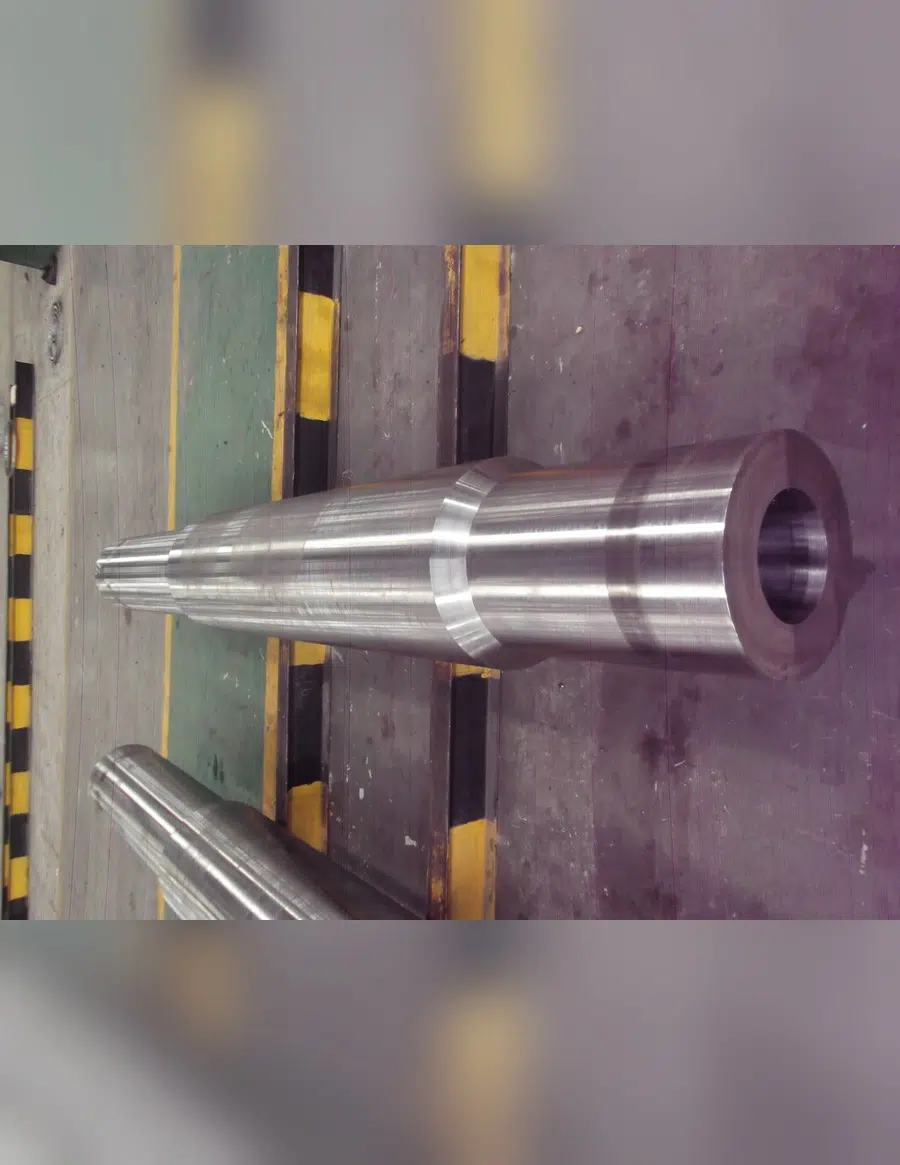
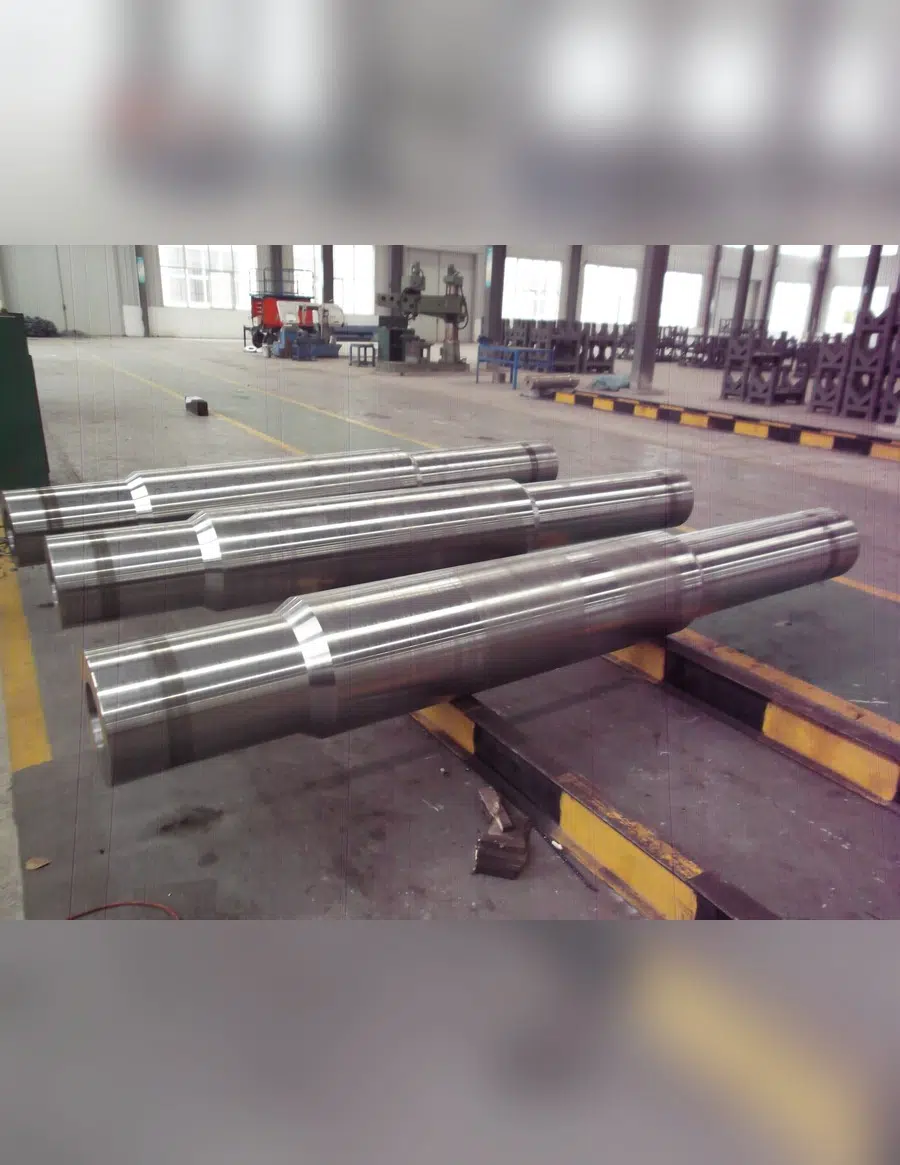
Forging route evidenceMachined-end detailBatch photo referenceMaterial discussion support
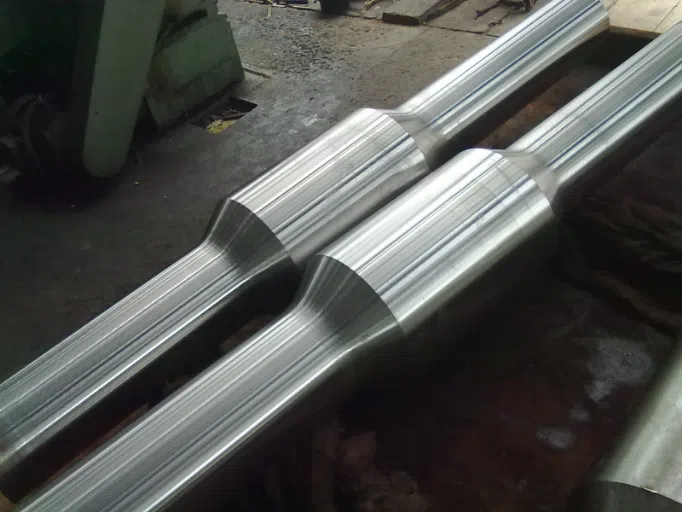
Forged vs Cast vs Machined Bar-Stock Shafts, Why Grain Flow Wins
ASTM A668/A668M is the primary U.S. specification for industrial-use carbon- and alloy steel steel forgings. It includes six classes of carbon steel and seven classes of alloy steel that are hot worked; unlike standards for other applications, the grades and test methods you choose should reflect your shaft’s intended use.
| Factor | Forged Shaft | Cast Shaft | Machined Bar Stock |
|---|---|---|---|
| Internal grain structure | Continuous, follows part contour | Randomly oriented on solidification | Continuous but cut across at steps/shoulders |
| Internal defects | Minimal when properly forged | Shrinkage porosity, gas voids possible | None from process, but fiber flow interrupted |
| Fatigue behavior under cyclic load | Improved by continuous grain flow | Weaker due to porosity and grain discontinuity | Weaker at re-entrant steps than an equivalent forging |
| Standard governing general use | ASTM A668/A668M (Class A–F carbon, G/H/J–N alloy) | Separate casting specs (e.g., ASTM A216/A217 families) | ASTM bar-stock specs (e.g., A29/A108 families) |
| Best suited for | High-cycle, high-torque rotating shafts | Complex shapes, lower-cycle static loads | Simple shapes, lower unit cost at small sizes |
No single one of these process is the one “right” answer – it’s a function of how the part will be loaded in service – after all, static housings or a cavity in a complex part might lend themselves well to casting if forging would be cost-prohibitive. But a shaft who take millions of cycles of load-time, transferring constant torque? That’s what forging is designed for – because grain-flow discontinuity – from a casting void, or from cutting across fiber-lines in a piece of barstock – is precisely the genesis of a fatigue crack.
A Note on Tolerance Expectations
The shape you forge is very close to net shape, but not to the finish size – the bar that arrives here goes on to CNC turning and grinding anyway. Specifying a finish-part tolerance like 0.01mm on the as-Forged surface won’t improve the final part quality but will increase your inspection costs for a surface that you’re going to machine off. We make the Forging allowance what your finishing operation requires.
“Buyers sometimes ask us to hold machined-part tolerances on the as-forged blank. We’d rather explain why that surface gets removed in turning than quote a number that just inflates the price without changing the finished shaft.”
Fewer Fatigue Replacements
Forged shafts’ continuous grain flow and lower internal-defect rate translate to fewer fatigue-related replacements over the service life versus cast alternatives — a pattern consistently reported across forging-industry engineering literature, though exact savings depend on your load profile and duty cycle.
Directional TCO pattern — industry engineering sources; not a Welong-specific measured figure. Request an application-specific assessment for your duty cycle.
An Honest Trade-Off, Not a Sales Pitch
We won’t suggest the choice between methods doesn’t come with its trade-offs. Making the jump from open-die to closed-die forging, isn’t a marketing compromise with a technical spin, it’s a compromise between tool-cost and the degree of shape, and where the laws of physics won’t bend to the grain-flow they’ll be told directly.
Ready to compare forging vs casting for your application?
Request a Custom Comparison →
Engineered for Power, Mining & Heavy Machinery Programs
What the shaft isn’t: in power generation, mining and heavy equipment-just some industries where rotating machinery is deployed-the single constraint in common is that the shaft can never be the cause of a line shutdown. As trade coverage of renewable-energy forgings and shipbuilding forgings both note, turbine rotor shafts transmit rotational energy from the blade or rotor stage into the generator, while mill main shafts and conveyor drive shafts carry sustained torque under abrasive, shock-loaded conditions.
Where Welong Forged Shafts Fit
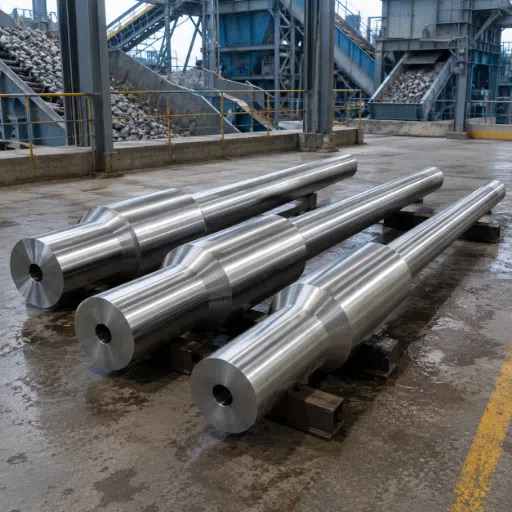
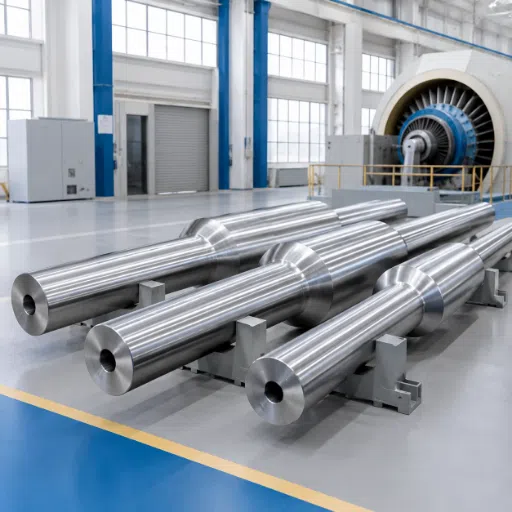
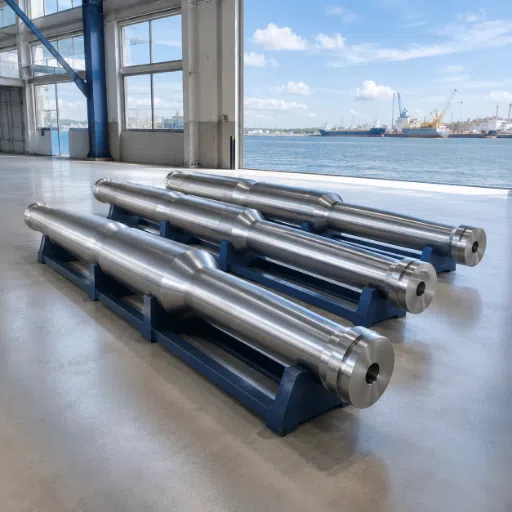
Our forging business is tied to our Mill Rolls division (work, backup, and pinch rolls for same steel-mill customer base), so a rolling-mill program can draw both main shafts and roll sets from one vendor relationship instead of two. And in each case, the basic reason for choosing forging remains the same: a rotating shaft operating for years under cyclic loading needs sustained internal grain flow, not a shape that simply look correct on the print.
Engineering Note, Diameter Threshold
According to some engineering support materials in the manufacturing field, as shaft diameter extends significantly beyond the sizes for rolled bar, forged blanks are preferred as forging aligns and refines grain of steel with the shaft shape – which is the geometry that support impact and cyclic loading in the service life. Don’t rely on a generic cutoff and confirm the applicable limit for your particular alloy and geometry by consulting our engineers.
Traceability & Batch Consistency
Material consistency issues in forged-part sourcing usually trace back to mixed heat numbers – batches that technically meet specifications but show minor composition or hardness variations from one production run to the next. Every Welong forged shaft is delivered with full material traceability by heat number and batch, and verified by independent third-party testing data (chemical composition, tensile strength, hardness), so your incoming inspection process won’t be guessing at consistency.
Certifications & Quality Control Stack
Every forged shaft is manufactured to a documented standard- not to a vague claim of “ISO certified” with no actual certificate. We produce to the specification your application truly requires, and we explicitly state so on our documentation.
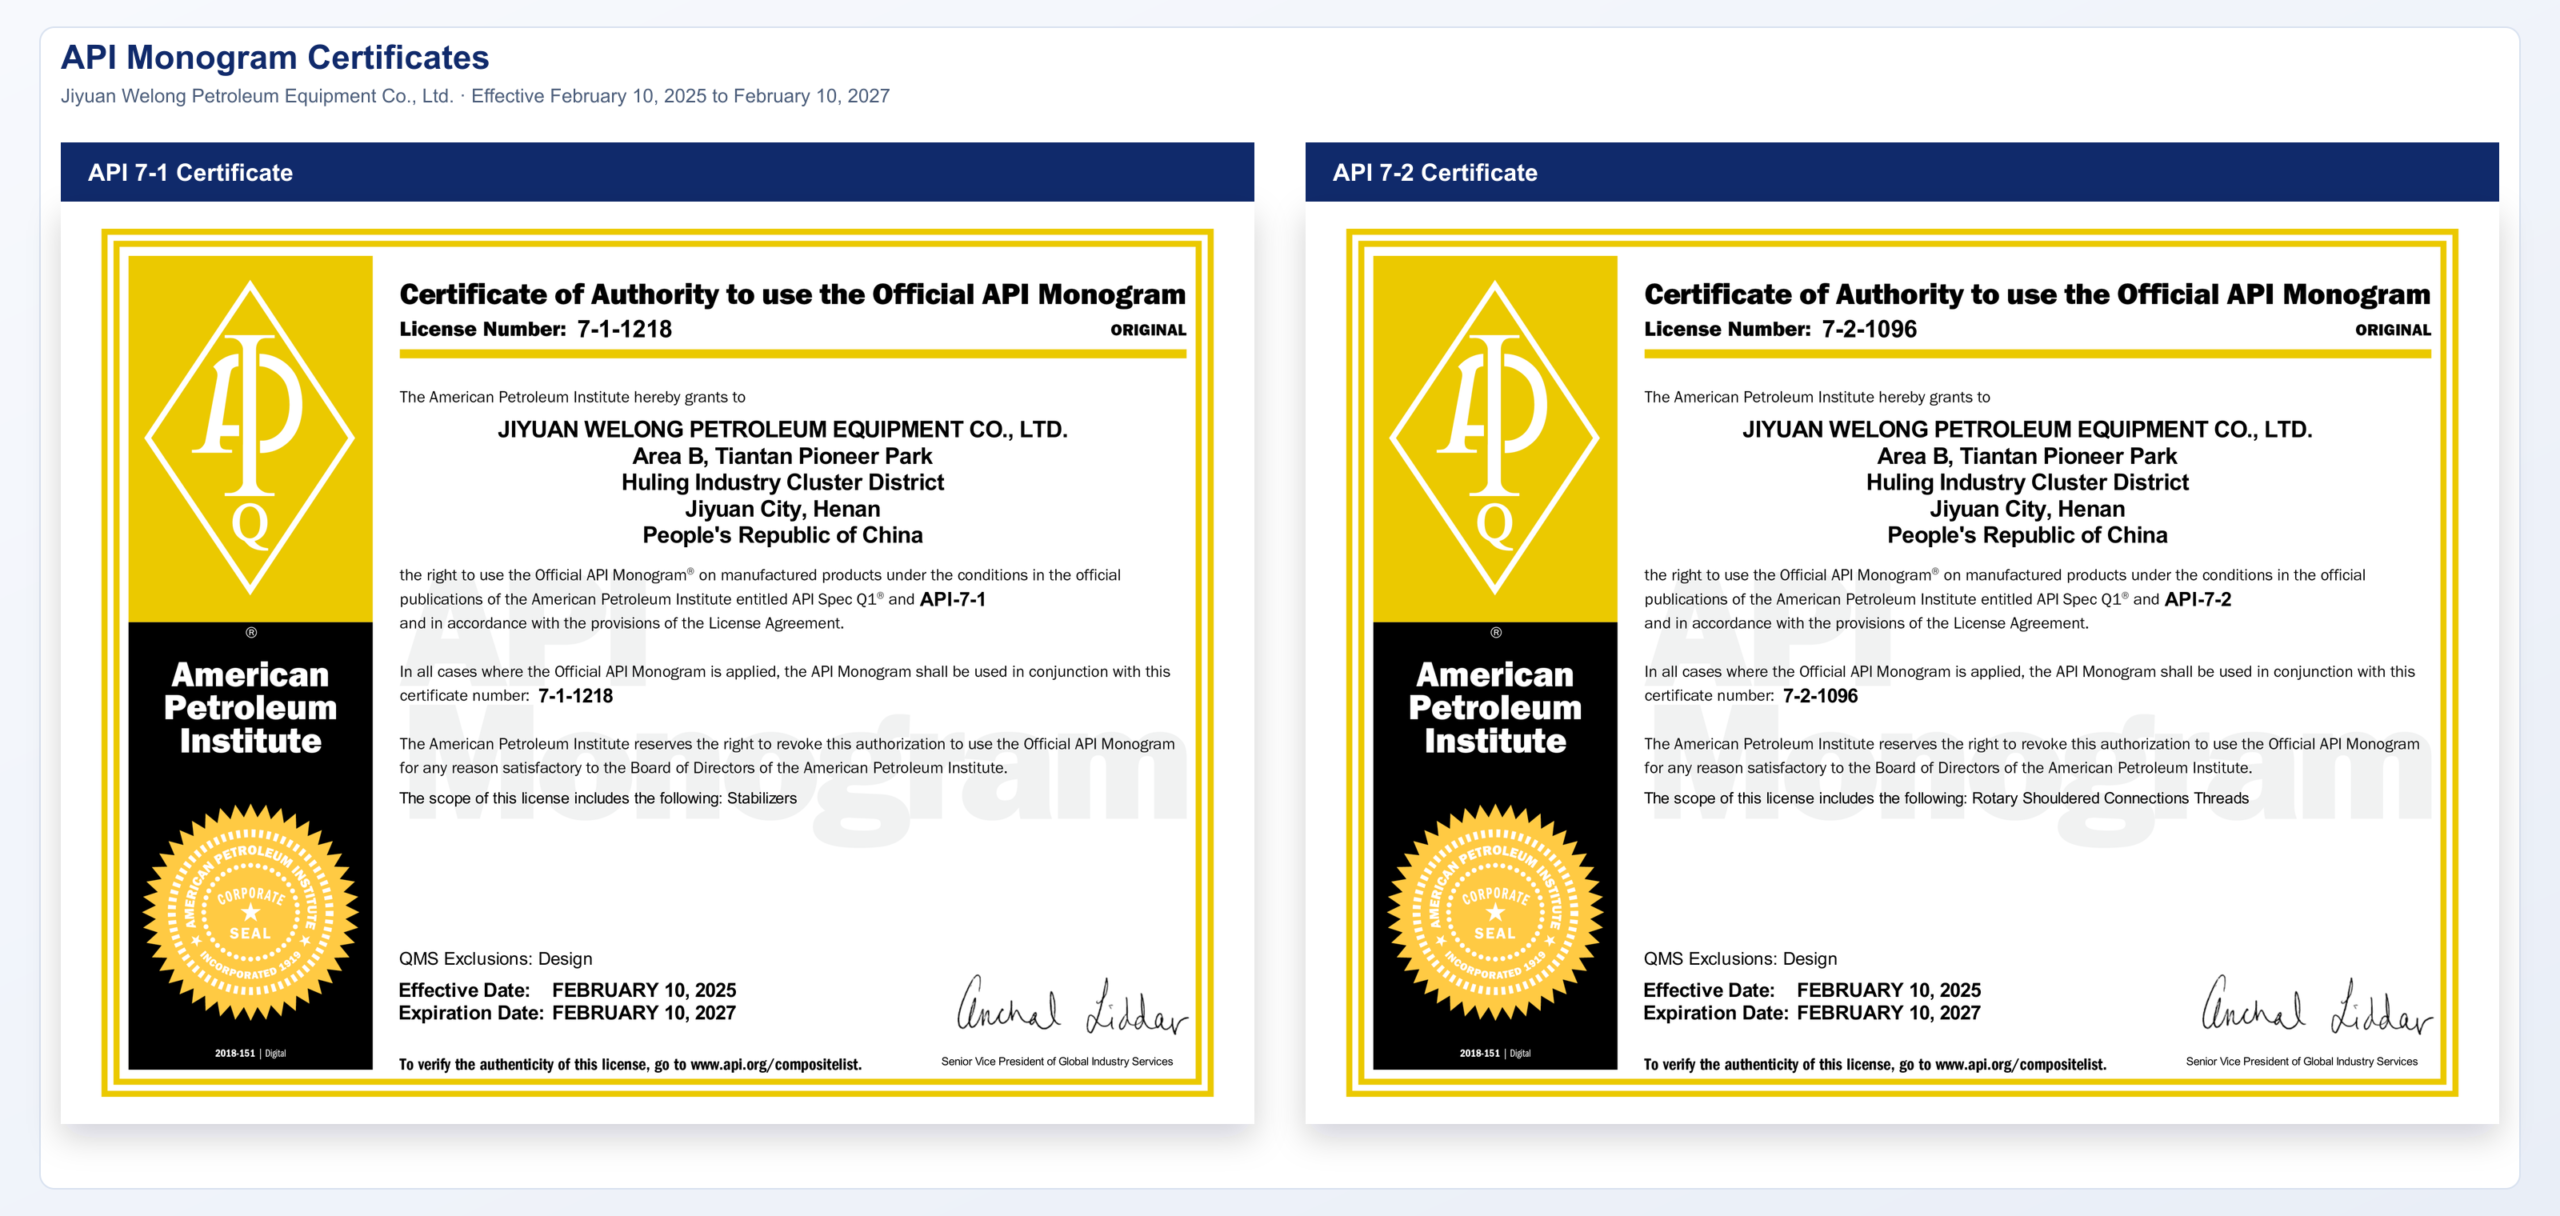
API
Oilfield & energy-grade specs
ANSI
US dimensional standards
ASTM A668/A668M
General industrial steel forgings
ASME
Mechanical engineering specs
DIN
German/European metric specs
GB
Chinese national standards
The grades identified as “equivalents” between API, ASME (BPVC Section II, Materials Part A), DIN, and GB are approximate: variations in chemical composition, mechanical property requirements, and delivery conditions can exist between standards even when both specify what appears to be the same alloy. We confirm the exact grade and standard per your drawing prior to beginning any forging.
Quality Control Test Stack (9 Methods)
- Chemical composition analysis
- Dimensional inspection
- Ultrasonic testing (UT)
- Magnetic particle testing (MT)
- Visual inspection
- Tensile testing
- Metallographic microscopy (grain structure verification)
- Impact (Charpy) testing
- Surface roughness measurement
Common Forging Defects We Screen For
Ultrasonic testing (UT)
A method to identify internal discontinuities, such as voids, inclusions, or forging bursts, that may not be visible on the surface.
Magnetic particle testing (MT)
Detects cracks on the surface or in the vicinity of the surface that could originate from an imprecisely controlled die transition or a poorly designed corner of a forged part.
Metallographic microscopy
Used to confirm that grain flow is indeed aligned with the contour of the part and not cutting across it; a critical verification for any shaft valued for fatigue strength.
Procurement Guide, Specifying, Lead Time & Ordering a Custom Forged Shaft
To speed up a forged shaft RFQ, please send us the three items below: (1) A dimensioned drawing of your part; (2) the required material grade or applicable standard, and (3) the final machining tolerance you require for critical diameter dimensions. We’ll address any other details- such as surface treatments, keyway or thread specs- against your drawing.
01
Drawing + material/standard review → forging feasibility confirmation
02
First-article sample forged, tested and machined for your approval
03
Bulk production scheduled once sample sign-off is complete
Pricing Factors & Cost Drivers
Weight class
Lighter and mid-range shaft sizes generally enter the production schedule faster than single large blanks.
Material
Standard carbon steel is quickest to obtain, while specialized alloy grades requiring particular heat-treating procedures may extend delivery time.
Scope of Testing
100% batch UT and MT is more time-consuming than sample testing but can help mitigate the risk of in-service failure.
Level of Machining
A finished-to-drawing product is obviously more costly and requires longer delivery than a part that’s only rough-turned.
Send us your drawing for a specific lead time on your particular configuration; we’d prefer to give you an accurate number for your actual requirement rather than a broad estimate that may not be applicable once your order is placed. Documentation You’ll Receive: Every order come with a mill test report (chemical analysis & mechanical properties by heat number, in the material-certification format ASME BPVC Section II, Part A defines for programs under that code), the appropriate NDT reports (UT/MT), and a dimensional inspection report against your drawing. If you’ve a program that require third-party witness inspection, we arrange for that while the shaft is still on the shop floor instead of after a disagreement arises.
Engineering Resources & Selection Tools
TOOL / CALCULATOR
Forging Method & Material Selector
Access Tool →
TECHNICAL GUIDE
Forged vs. Cast vs. Machined Bar-Stock — Factor by Factor
Read Guide →
PROCUREMENT CHECKLIST
RFQ Readiness Checklist
View Checklist →
SPECIFICATION
Quality Control Test Stack — What Each Method Verifies
Review Specs →
FAQ
What is a forged shaft, and how is it different from a cast or machined one?
A forged shaft is formed under compressive plastic deformation which means that the steel grain structure is continuous through out the part instead of being randomly oriented like a casting, or having its fibers cut at steps like a bar-stock machine part. Continuous grain flow is the single reason forged shafts stand up better under cyclic torque and bending loads.
What material is used for forged shafts?
Carbon steel (42CrMo4, 4140, 4340 and others), stainless steel, alloy steel, aluminum alloy, copper alloy, titanium and zirconium-selected to meet your load, environmental, and standard requirements.
Are forged parts stronger than cast or machined parts?
Under cyclic and impact loading, yes-the continuous grain flow in a forging generally outperforms the randomly oriented grains of a casting, or the interrupted fiber flow of a machined bar-stock component. In static, low-cycle service the difference isn’t significant, and that’s why casting or bar-stock can be the most economical choice outside high-cycle, rotating shaft duty.
Why does the forged blank tolerance look wider than my finished-part drawing?
Forging produces a near-net shape, not a finished dimension, and the part still receives CNC turning and grinding after it leaves the forge. Calling out a finished-part tolerance on a surface that get machined away adds cost without improving performance-we size the forging allowance to match what your subsequent machining will actually remove.
How do I know I’m getting consistent material quality across production batches?
Ask for traceability by heat number and batch, along with third-party validated chemical analysis, tensile, and hardness data-that’s what catches the variations that occur between batches, even when they’re nominally “in spec.” Every Welong forged shaft is delivered with that data.
What should I watch for when evaluating a forging supplier?
Vague answers are the tell: a supplier who says “we’ll do our best” on delivery time, or “it should be about right” on tolerances, hasn’t committed to anything you can hold them to. Ask for an exact lead time against your drawing, not a broad estimate.
Are forged shafts more expensive than cast or machined-bar alternatives?
Don’t base a price comparison on unit cost only. Total cost of ownership considers replacement frequency, unexpected downtime, and collateral damage from a failure, not just the purchase price. forged shafts cost more upfront, but less frequently fail under cycling load-why they’re preferred for critical rotating equipment.
What size range can Welong supply?
Our forging and casting divisions support part weights between 0.2 and 50 tons. Review our current forging schedule with your specific shaft dimensions and weight before you submit a drawing to us, because our capabilities can vary based on part configuration and material grade.
Do you supply forged shafts to standards other than ASTM?
Yes, to include API, ANSI, ASME, DIN, GB and ASTM A668/A668M standards. Standards equivalency should always be verified against your drawing prior to placing the forging order because there are no precise standard equivalencies.
Can you supply hollow-bored or flanged shafts?
Yes. shafts that need to be lighter, or carry fluid are hollow-bored using forged and boring, while shafts with integral flanges are forged as a single piece (forged), and don’t include a weld in the load path.
What surface treatments are available?
Finishes – Steel-proofing, paint, galvanization, powder coating – all defined to your operating, transit, and in-use conditions. If needed on your print/PO, they’ll be added to your forgings/finishing schedule.
Open die vs closed die forging, which should I specify for my shaft?
Open-die forging is our usual process for big and somewhat-flat shafts, and most shafts that resemble steps (closed dies don’t generally pay for themselves on low-volume or extra-large parts), and when we recommend we go against your print/order – we’re not going to default to open or closed die.
Procurement & Capability
Forged Shafts Capability Review
China Welong reviews the buyer drawing, product specification and inspection scope before quotation.
24 hEngineer-reviewed quotation on business days
2001Founded in 2001
30+30+ engineers on staff
5 yrStamped serial traceability
Quotation Scope and Commercial Terms
Pricing is prepared against the selected product configuration, material route, inspection scope and shipment terms.
- Quotes are returned within 24 hours on business days, reviewed by an engineer.
- T/T or L/C by wire transfer.
- We ship EXW, FOB, CFR or CIF; other Incoterms on request.
- We work from 2D drawings and 3D CAD models (AutoCAD, Pro/ENGINEER, SolidWorks; .dwg and .igs).
Production Planning
Production timing is confirmed with the quotation after quantity, process route and finishing scope are reviewed.
- We hold agreed items in stock and ship against your release to shorten delivery. Feasibility is confirmed at drawing review.
- Manufacturing at Xi'an, Shaanxi and at Jiyuan, Henan.
- 0.01 mm machining precision.
- Material standards to ISO, BS, ASTM, ASME, DIN, JIS and GB.
- Orders ship in standard export wooden cases, or the packing you specify.
Order Review and Responsibility
The responsible manufacturer, inspection scope and document package are identified for the selected item.
- Every quotation states whether the item is made in our own works or by an approved supplier we developed and supervise.
- We develop, audit and supervise the mills and workshops that make your parts: material mills are re-audited every two years and approved by Welong before they run your order.
- Centrifugal castings to 3,000 kg, 4,000 mm long, 2,000 mm outside diameter, 8 mm minimum wall.
- Forgings from 0.2 to 50 tons.
Specification and Inspection Evidence
The specification table on this page is the technical basis for this review: its numeric rows define what we quote, manufacture and inspect against.
- Each piece carries a stamped serial number and stays traceable for five years to its chemical composition, mechanical properties and measurement report, with the test coupon retained.
- An EN 10204-3.1B material certificate with chemical composition and mechanical properties, a dimensional measurement report, and UT and MT reports ship with your order.
- Inspection is by coordinate measuring machine, ultrasonic, magnetic particle and X-ray.
Five rows reproduce current-page wording; four legacy first-party rows reproduce the old Welong shaft-forging page and are identified row by row in the batch ledger. The quotation confirms the responsible manufacturer and inspection scope for the selected item.
| Parameter | Evidence wording |
|---|---|
| Forging weight range | The scope of weight | 0.2-50 tons |
| Shaft forging material grade | Shaft Forging: 42CrMo4+QT |
| Alloy steel grade families | Alloy steel (42CrMo4 / 4140 / 4340) — high hardenability, fatigue resistance after Q&T |
| Governing shaft-forging standard | ASTM A668/A668M (Class A–F carbon, G/H/J–N alloy) |
| Non-destructive testing scope | 100% batch UT and MT |
| Machining precision | 0.01 mm machining precision |
| Legacy first-party inspection sequence | Chemical composition inspection + Dimensional inspection + UT testing + MT testing + Visual inspection |
| Legacy first-party material standards | API, ANSI, ASTM, ASME, DIN, GB |
| Legacy first-party process route | Forging / Heat Treatment / Machining |
Request a Product Review
Send the drawing, product specification and inspection requirements for a quotation review.